
Core assembly is the most labor-intensive stage in a plywood mill that has not yet automated. Workers align narrow veneer strips edge to edge, trim the ends, apply glue or tape, cut to length and stack the sheet — and the quality of the result depends on how well each person does it on each shift. A core veneer composer replaces that manual sequence with servo positioning, trimming and automatic stacking, turning a skill-dependent process into a repeatable one.
This guide explains what the machine does, how the horizontal and L-type models differ, what output and quality to expect, and how to match a composer to the dryer and press that surround it.

Why Manual Lay-up Becomes the Bottleneck
Manual core assembly has three structural problems.
It does not scale linearly. Adding output means adding workers, floor space and supervision. Beyond a certain point, more people create more coordination work rather than more panels.
Quality depends on the operator. A gap between strips creates a low-density zone; an overlap creates a high spot. Both show up later as thickness variation, glue starvation, press marks or delamination. The same crew can produce acceptable panels in the morning and rejects after a shift change.
It is hard to staff. Core assembly is repetitive, physical work. In markets where wages are rising and turnover is high, keeping an experienced lay-up crew is a persistent management problem — and a mill that depends on one experienced team carries operational risk.
Automation does not eliminate the operator. It moves the operator from aligning strips by hand to supervising the machine and checking quality.
What a Core Veneer Composer Actually Does
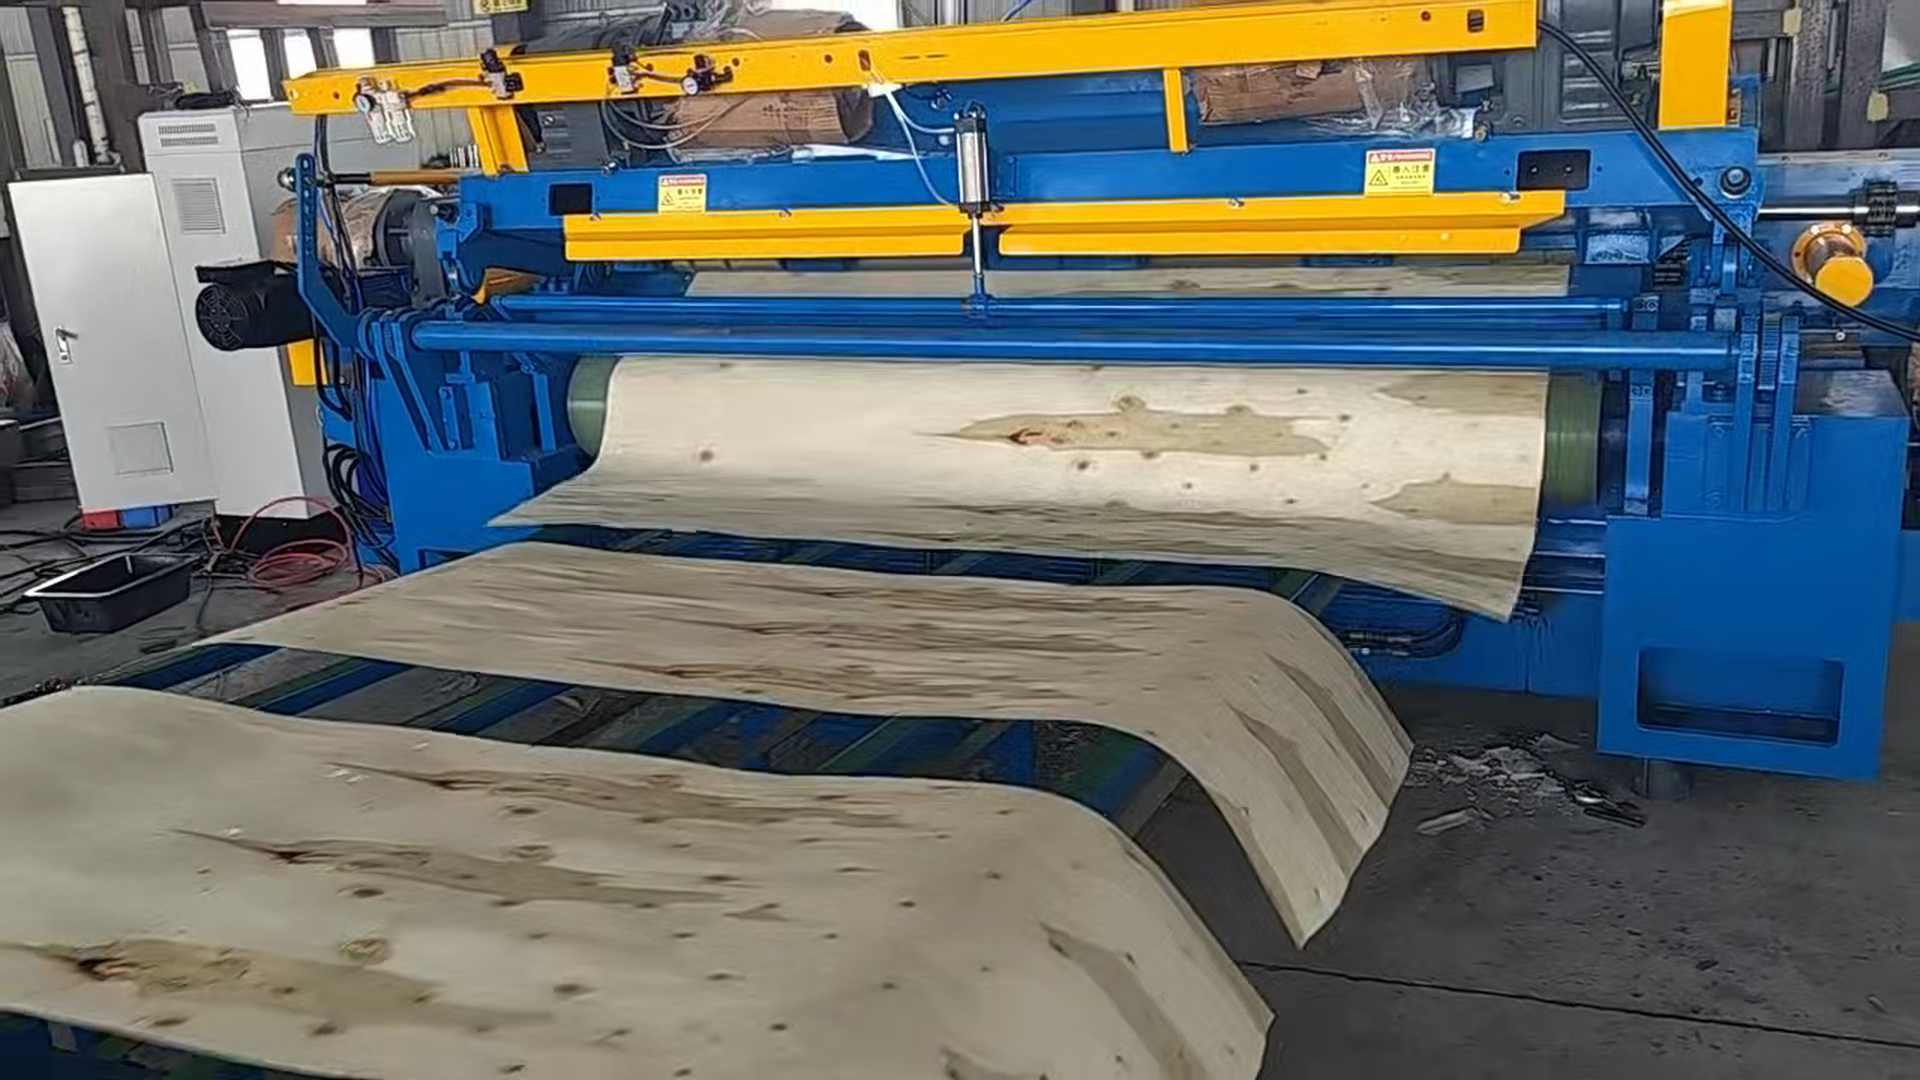
The machine performs a sequence: feed the veneer strips, trim the edges square, apply adhesive, join the strips edge to edge, cut the assembled sheet to length, and stack the finished core panel.
Horizontal composer
Our horizontal model DHPB-5A1 is the standard choice for core veneer production:
| Parameter | Specification |
|---|---|
| Veneer thickness | 1.0–3.6 مم |
| Joining direction | أفقي |
| Conveying speed | 0–35 m/min, adjustable |
| Output | 300–360 finished panels per hour |
| الطاقة الإجمالية | 35 كيلوواط |
| Machine weight | 5500 kg |
| Complete line dimensions | 12,500 × 4,000 × 2,480 مم |
| Composer dimensions | 4,040 × 2,510 × 1,960 مم |
| Stacker dimensions | 3,400 × 2,200 × 2,480 مم |
| Knife length | 1400 mm |
| Glue tank heating | 9 كيلوواط |
| Servo drives | 3 kW SINEE for front/rear drive, trimming and length cutting |
| Control | TECO PLC with WECON touchscreen and remote support |
| Stacker lift | 2.2 kW × 2 |
The glue tank is heated, which helps keep adhesive flow consistent through the roller system. The stacker is integrated into the line, so the finished core sheets leave the machine in a stack rather than in a loose pile that has to be handled again.
L-type composer with finger jointing
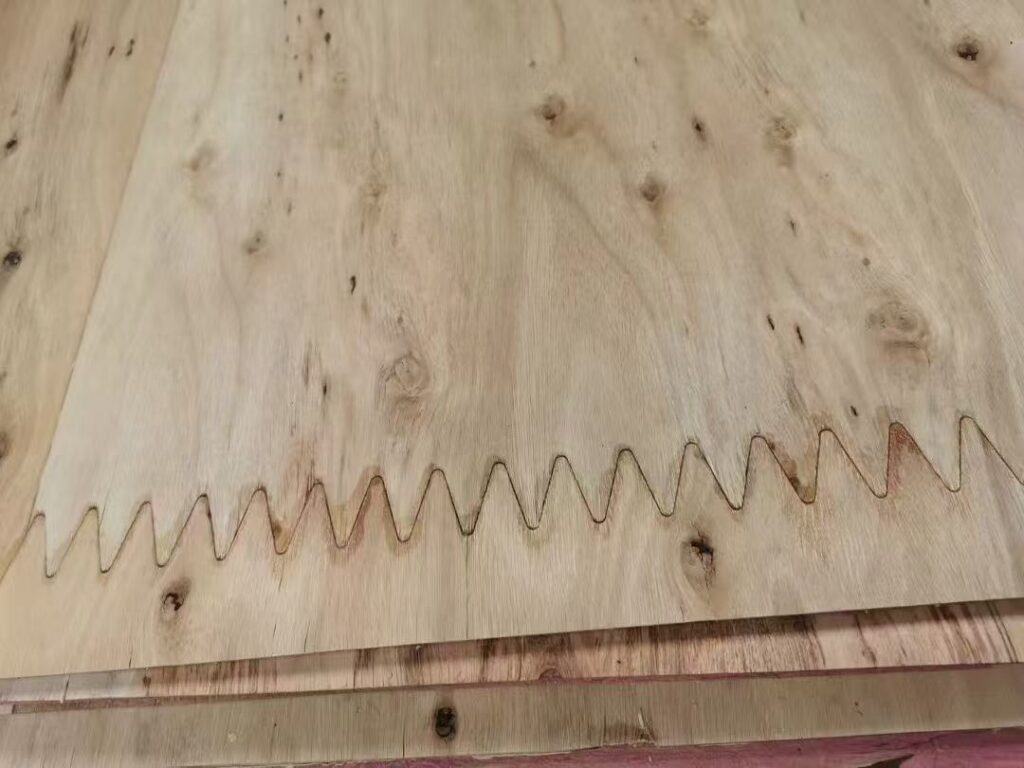
The L-type model DHPB-5A1-L adds longitudinal finger jointing to the horizontal join. That allows the mill to produce wider core sheets from shorter pieces and to use offcuts that would otherwise be downgraded.
| Parameter | Specification |
|---|---|
| Veneer thickness | 1.5–4.0 mm |
| Joining direction | Horizontal plus longitudinal |
| Finger joint size | 30 × 30 mm, 42 fingers per joint |
| Output | About 300 panels per hour |
| الطاقة الإجمالية | 64.6 kW |
| Machine weight | 9500 كجم |
| Finger-joint section | 16 mm steel plate |
| Longitudinal servo drives | 3 × 3 kW SINEE |
| Hydraulic finger-joint knife | 11 كيلوواط |
| Control | TECO PLC with WECON touchscreen |
The L-type is the right choice when raw material cost matters more than machine simplicity — for example, when the mill gets a significant share of short or narrow veneer that would otherwise become waste.
Small strip composer and paving line
For mills producing smaller core formats, the small strip core composer covers 1.2–4.0 mm veneer and outputs 4 × 4 ft or 4 × 8 ft sheets at a line speed of 3–4 sheets per minute. It uses 18 kW total power and weighs about 4 t, making it a lighter entry point than the full horizontal line.
The core veneer paving line is a different tool for the same problem. It does not join strips; it automates the alignment and lay-up of core veneer before pressing. The line is 30 m long — 24 m of conveying plus the cutting section — with 13.5 kW total power and a weight of 5.6 t. Its value is preventing gaps, overlap and misalignment before the assembly reaches the press.
Output and Quality: What Automation Actually Changes
| Model | Veneer thickness | Output | الطاقة الإجمالية | الوزن |
|---|---|---|---|---|
| Horizontal composer DHPB-5A1 | 1.0–3.6 مم | 300–360 panels/hour | 35 كيلوواط | 5500 kg |
| L-type composer DHPB-5A1-L | 1.5–4.0 mm | About 300 panels/hour | 64.6 kW | 9500 كجم |
| Small strip composer | 1.2–4.0 مم | 3–4 sheets/minute | 18 kW | About 4 t |
| Core veneer paving line | Depends on line | Lay-up and alignment | 13.5 kW | 5.6 t |
The quality improvement comes from three mechanisms:
- Servo positioning keeps the strips aligned to the same reference, sheet after sheet.
- Trimming before joining produces square edges, so the joint is tight rather than forced.
- Integrated stacking prevents the sheets from shifting after assembly, which protects the joint before pressing.
The result is a core panel with tighter seams, fewer gaps and overlaps, and more consistent thickness — the conditions that make the downstream press and sander predictable.
Labor and Training: What Changes on the Floor
The machine does not remove people from the line. It changes what they do.
In a manual layout, several workers handle alignment, trimming, gluing and stacking in sequence. With an automatic composer, the crew shifts toward feeding, quality inspection, glue supply and stack removal. The physical pace is set by the machine, which makes output more predictable and reduces the variation between shifts.
Training is shorter than it looks because the interface is a PLC with a touchscreen. Operators need to understand thickness settings, glue supply, stack height and basic fault recovery. Remote support allows the supplier to help diagnose settings without waiting for a site visit.
The exact labor reduction depends on your current layout, panel size and shift pattern, so it should be measured against your own line. To be confirmed for your factory.
Case Examples: Vietnam and Indonesia
Vietnam: three composers replacing manual assembly
A medium-sized Vietnamese plywood factory had relied on manual core veneer assembly for years. Rising labor costs and customer demand for more consistent panel quality pushed the owner to automate.
We recommended a 30 m automatic core assembly system — a 24 m feeding conveyor plus a cutting and pressing platform — and the customer purchased three automatic core composers. The machines were completed in 20 days, and after installation the factory reported:
- Production efficiency increased by more than 50%
- Core panel quality became more consistent, with tighter bonding
- Fewer workers were needed, and workflow management became simpler
Indonesia: fully automatic core assembly in an export plant
A larger Indonesian producer building a new export-oriented factory at a designed output of 150 m³ per day included a fully automatic core composer in the line. The machine uses an advanced conveyor and positioning system with automatic joint adjustment, so joints stay tight and even with minimal manual intervention. The plant also runs a 30-layer fully automatic hot press and a fully automatic sanding line, which is the configuration that makes sense when output and export quality are both priorities.
Both results are project-specific. Your output, species and panel format will determine the actual gain.
Matching the Composer to Your Dryer and Press
A composer is a throughput stage, and it has to fit the stages around it.
- Veneer thickness range. The horizontal model covers 1.0–3.6 mm, the L-type 1.5–4.0 mm and the small strip model 1.2–4.0 mm. Choose a machine that covers your actual production range, not just your current product.
- Output match. 300–360 panels per hour sounds high, but the real constraint is often how fast the dryer and press can absorb the panels. Match the composer to the press cycle rather than buying the fastest machine available.
- Panel format. The small strip composer produces 4 × 4 ft and 4 × 8 ft sheets. If you need wider core sheets or want to use short offcuts, the L-type finger-joint model is the relevant option.
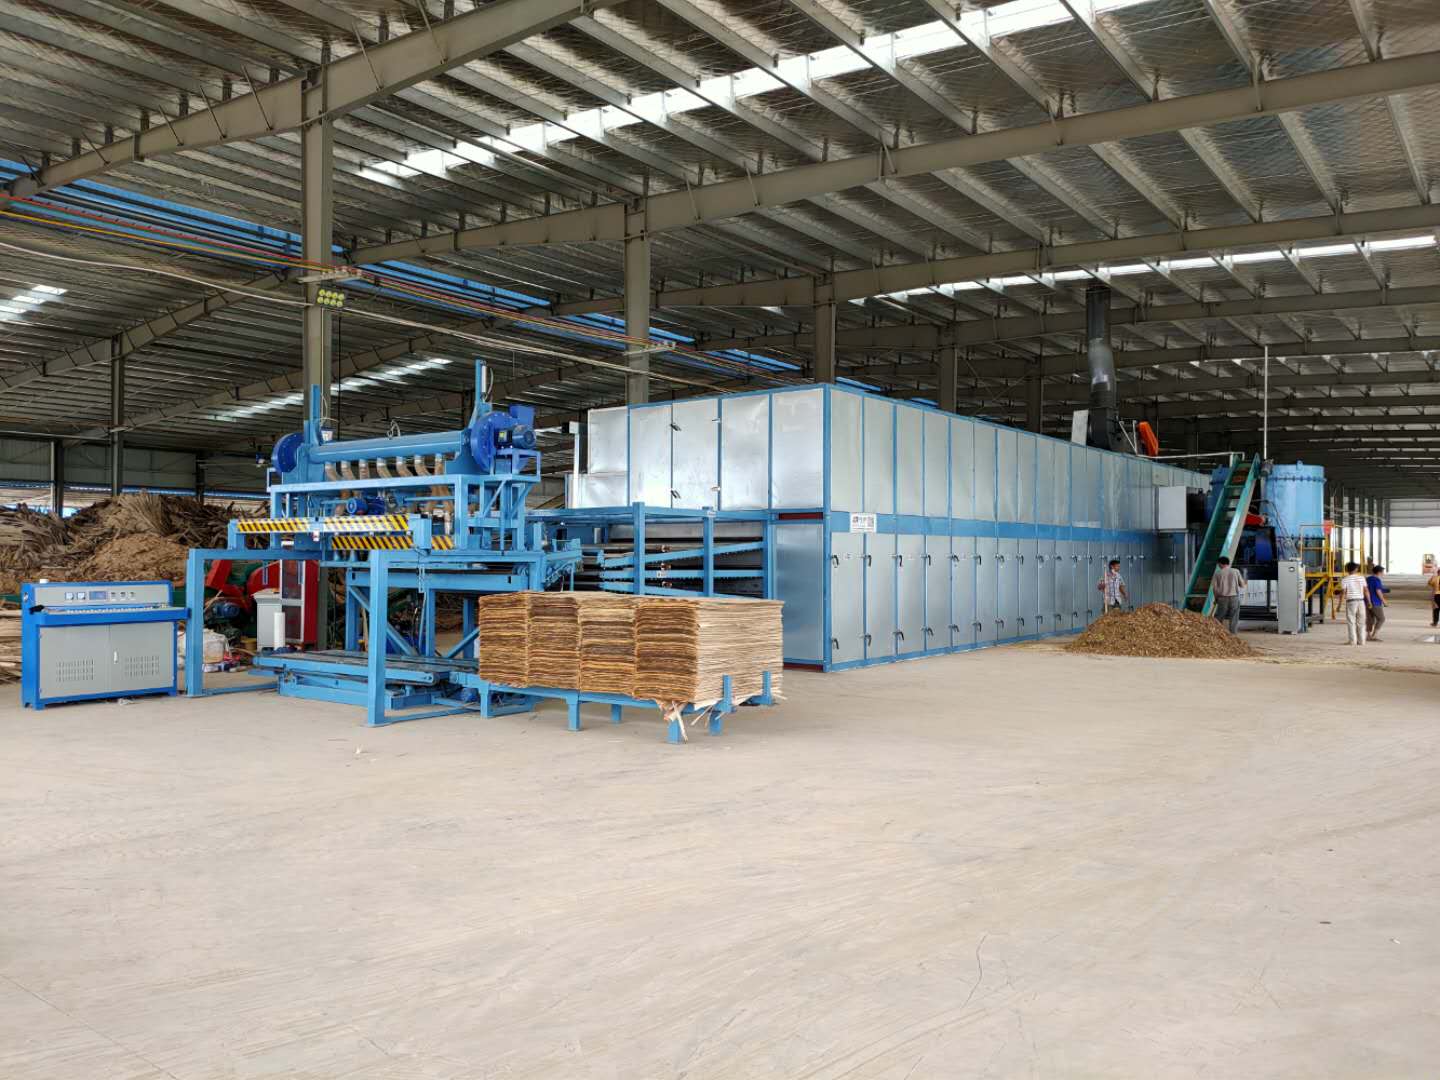
- Floor space. The horizontal line is 12.5 m long; the L-type is built from separate horizontal, longitudinal and stacking sections. Check the layout against your building before ordering.
- Glue and curing. The composer applies adhesive, and the assembly must reach the press within the working time of the glue system. Confirm the adhesive’s open time and the distance to the press as part of the layout.
الأسئلة المتكررة
What does the machine do?
It joins narrow veneer strips into a continuous core sheet: trimming the edges, applying adhesive, joining the strips, cutting to length and stacking the finished panel. It replaces the manual lay-up sequence with a servo-controlled process.
What is the difference between a horizontal composer and an L-type composer?
The horizontal model joins strips edge to edge in one direction. The L-type adds longitudinal finger jointing — 30 × 30 mm fingers, 42 per joint — so it can produce wider core sheets and use shorter offcuts.
How many panels can it produce?
The horizontal DHPB-5A1 is specified at 300–360 finished panels per hour, the L-type at about 300 panels per hour, and the small strip composer at 3–4 sheets per minute. Actual output depends on veneer thickness, panel size and how quickly the line removes the stacks.
Can it handle thin veneer?
Yes. The horizontal model covers 1.0–3.6 mm, the L-type 1.5–4.0 mm and the small strip composer 1.2–4.0 mm. Confirm the lower limit against the thinnest veneer you actually run.
How much labor can it replace?
It removes manual alignment and joining, but the exact headcount reduction depends on your layout, panel size and shift pattern. In a Vietnamese project, the customer reported more than 50% higher production efficiency and fewer workers after replacing manual assembly with three automatic composers.
Next Step: Match the Composer to Your Output
The right core veneer composer is defined by your veneer thickness range, panel format, target output and the space between the dryer and the press. Send us those details, along with your current labor layout, and our engineers will recommend the model, line length and stacking configuration, usually within 48 hours.
Review our core assembly systems here: www.guoyumachine.com/product-category/plywood-making-machine/core-composer